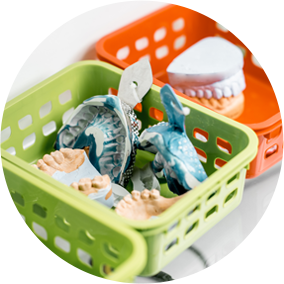
A storage container looks like one of the simpler things a mold can produce — no moving parts, no visible cosmetic panel, just a box that needs to hold what goes inside it. That simplicity is deceptive. Plastic storage products are usually made in multi-cavity molds running four, eight, or more cavities per cycle, and getting every one of those cavities to fill and seal identically is a harder problem than the finished part suggests. The mold, not the part design, ends up carrying most of the difficulty.
High-volume plastic storage products rarely come from single-cavity tooling, since per-part cost at scale depends heavily on how many parts a single machine cycle can produce. Adding cavities lowers cost per unit, but each additional cavity increases the risk of uneven filling if the runner system and gate placement are not balanced carefully. A cavity positioned slightly farther from the sprue can fill a fraction of a second later than the others, which is enough to create subtle dimensional or wall-thickness differences across what is supposed to be an identical part.
Where plastic storage products need to hold contents securely — a lidded container, a sealed box, a container with a gasketed closure — the fit between mating surfaces has to be dialed in at the mold level rather than corrected afterward. A silicone gasket molded directly into a lid, for example, needs a cavity geometry precise enough that the gasket seats into a continuous channel rather than a series of slightly misaligned segments. Getting this right in the tool avoids a downstream assembly step and produces a more consistent seal than fitting a separately molded gasket by hand.
The plastic behind plastic storage products varies by end use more than buyers sometimes expect. Rotational molding with UV-stabilized polyethylene suits large, hollow items like planters that need to hold their shape outdoors, while injection-molded polypropylene is more common for smaller containers where wall thickness and cycle time matter more than single-piece hollow strength. A flexible polymer blend, used in some fitting-style products, allows slight expansion under stress — such as when contents freeze — without the part cracking, which is a different design goal entirely from the rigidity a stackable storage bin needs. Getting this choice wrong rarely shows up in early testing; it tends to surface only after repeated cycles of the exact stress the material was meant to handle.
Because multi-cavity tools for plastic storage products run continuously at volume, cooling channel placement has an outsized effect on daily output. Cooling that removes heat unevenly across cavities extends cycle time for the whole tool, since production has to wait for the slowest-cooling cavity before the next shot can begin. Balancing this across every cavity in a high-cavitation mold is one of the less visible parts of the design process, but it is often what separates a tool that hits its target output from one that consistently runs behind schedule. For buyers evaluating a supplier's capability, this cavity-and-cooling balance is frequently a better indicator of how reliably plastic storage products will ship on schedule than the cavity count alone.
For distributors and product developers sourcing this category, useful comparison points include cavity count relative to target production volume, gasket or seal integration method where a closure is required, material selection relative to intended use (indoor versus outdoor, rigid versus flexible), and how consistently wall thickness holds across every cavity in a production run rather than just a sample part. Taizhou Huangyan Bonuo Mould Co., Ltd., producing daily-use plastic product tooling from its Huangyan District facility in Taizhou, works across this range of cavity counts and material types, giving buyers a way to compare plastic storage products tooling options against the specific volume and sealing requirements of their own product line.


Product Categories
Contact Us

+86-13586020128

No. 118, Xiangnv Road, Chengjiang Street, Huangyan District, Taizhou City, Zhejiang Province, China
Ready to Begin?
Get in Touch

Now!

BONUO
 English
 русский
 Español
 عربى

